Multi-channel testing
Choose 4- or 8-channel configurations, with channel quantity and fixture design tailored to the product and throughput requirement.
 ASPI IndustrialPrecision solutions
Water-bath / steel-ball
A multi-channel insulation testing platform built around the manufacturer’s product. One operator runs it, which reduces manual verification error; throughput and optional data traceability follow the delivered configuration.
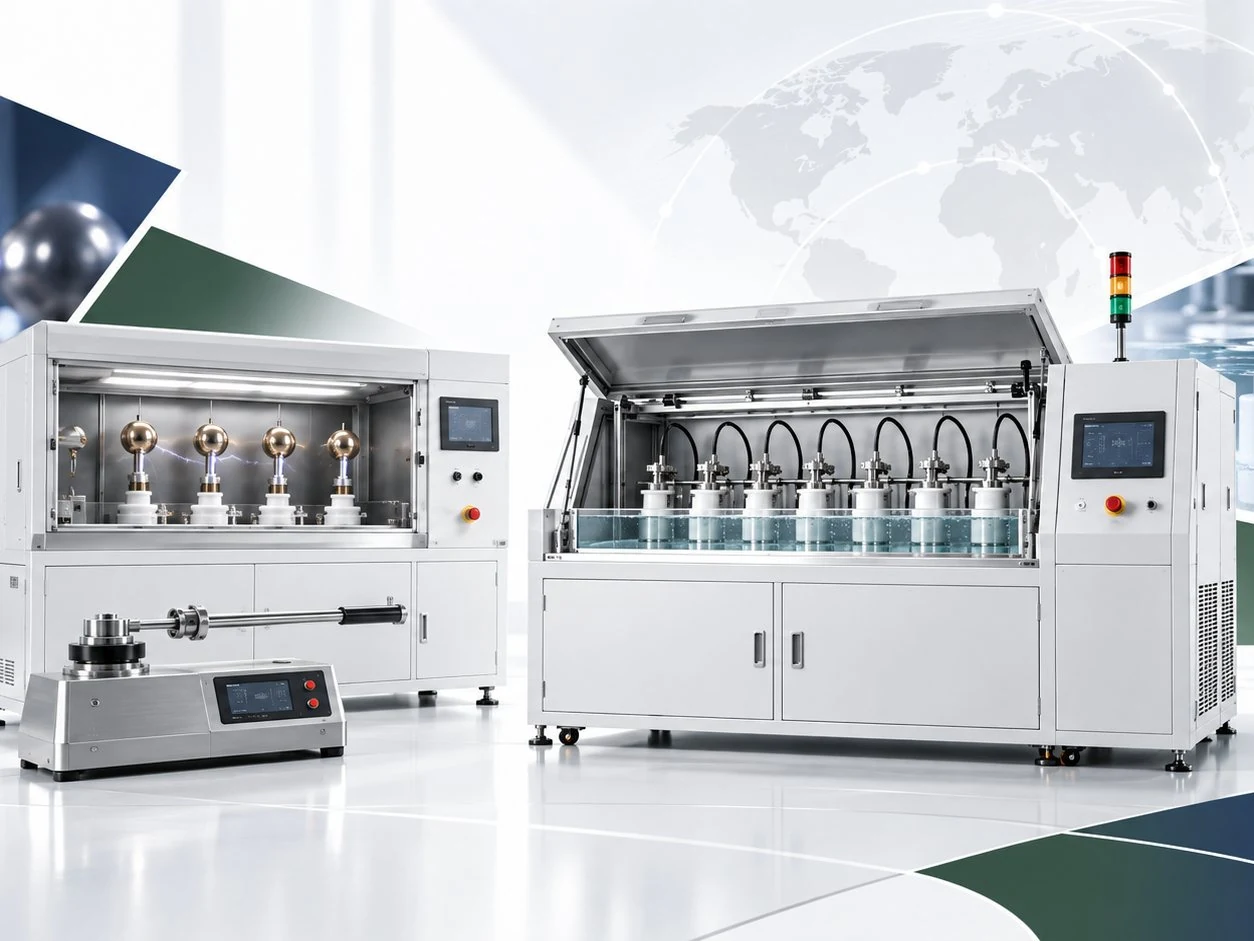
A configurable inspection platform
Choose 4- or 8-channel configurations, with channel quantity and fixture design tailored to the product and throughput requirement.
Supports AC testing from 100 V to 10,000 V, subject to final application configuration.
A standardized semi-automatic method helps reduce manual calibration and operating errors.
Optional SQL retrieval, statistics, analysis, real-time display, and role-based account permissions support traceable records.
Application and workflow
The system is intended for products that require high-voltage insulation testing within a controlled, operator-oriented production sequence. Fixture design and the exact loading method remain application-specific.
Position the product in the configured fixture.
Run the defined multi-channel high-voltage sequence.
Review the configured result and pass/fail outcome.
Store or retrieve results when optional data functions are specified.
Technical snapshot
Final performance, fixture design, cycle time, and configuration must be confirmed against the buyer’s product and testing requirements.
Model finder
All three standard configurations share the same test voltage range (AC 100–10,000 V, guaranteed 1,000–10,000 V) and test method — the real difference is channel count and throughput. Pick a use case, or enter a target throughput, to see a suggested configuration.
Pick a use case or enter a target throughput to see a recommendation.
Lab R&D and sample testing
1 channel · project-specific configuration
Low-volume, non-continuous verification work — suited to R&D sampling or first-article checks.
Discuss specs with usHand-tool QC / sampling inspection
4 channels · 45-second cycle · up to 320 pcs/hour
A common choice with mixed models, frequent changeover, or limited floor width.
View quick specHand-tool production line / high-throughput inspection
8 channels · 30-second cycle · up to 960 pcs/hour
A common choice when volume on a single model is high and output is the governing condition.
View quick spec320 / 960 pcs per hour is a full-load conversion from the standard cycle; actual throughput is still confirmed against the sample part and the production condition.
We also offer a custom fully automatic water-bath insulation tester, with configurations tailored to different requirements. Specifications are provided after the project is discussed. Discuss a custom requirement
Channel count affects cycle, footprint and output at the same time. The table compares the two standard configurations for a first pass; fixture design and the actual loading method still depend on the sample part.
| Item | 4-channel | 8-channel |
|---|---|---|
| Standard cycle | 45 seconds | 30 seconds |
| Full-load conversion | Up to 320 pcs/hour | Up to 960 pcs/hour |
| Machine size (W×D×H) | 1,500 × 1,100 × 1,900 mm | 2,000 × 900 × 1,900 mm |
| Net weight | 600 kg | 800 kg |
| Typical selection case | Mixed models with frequent changeover; limited floor width | High volume on a single model; output is the governing condition |
320 / 960 pcs per hour is a full-load conversion from the standard cycle, not a verified production output. Real hourly output must also account for loading, retesting and downtime; if the specified test method requires a longer dwell (three minutes, for example), the 30/45-second cycle cannot be reused for the conversion. Final throughput is confirmed against the sample part and the production condition.
See it in action
The video shows the equipment running in a production-test setting. Actual test methods, parameters and acceptance conditions follow the specified standard, tool category and delivered configuration.
A calibration report is key evidence for measurement capability, but it has to be read in full. Check at least these seven items, and confirm they cover the acceptance threshold you actually use.
Resolution is the smallest increment the equipment can display. Even where the reading error at a calibration point is small, the expanded uncertainty stated in the report and the actual operating conditions still apply.
A calibration report, a test report executed to a standard, and third-party product certification are three different kinds of evidence. Where a purchase contract requires VDE or another certification, the certified product, the certificate and its scope have to be checked separately.
A calibration report is issued per machine: one report covers that serial number, that date and the calibration points listed in it, and cannot be read as performance across the series. Specify the channels, frequencies, measurement points and uncertainty you need at the enquiry stage, and confirm the report fields against your own QA system. Calibration reports for delivered machines belong to that buyer and are not shared.
These are the questions buyers most often need answered outside the datasheet — on selection, rollout and preparing for a VDE factory inspection.
No. Applying a standard method, presenting test results and obtaining third-party certification each require their own evidence. We can confirm the equipment configuration and test method with you against the specified clauses first; where VDE certification is required, check the certified product, the certificate and its scope separately.
Not on their own. Tool category, test stage, fixture, test duration, pass/fail criteria and measurement evidence need to be confirmed together. If you send a representative sample part and the standard edition, we can move to a specific configuration faster.
Please provide plant location, site power supply and protection system data, installation environment, sample parts and intended use. We use these with your locally qualified electrical professional to confirm installation and verification items, and agree responsibilities and deliverables on both sides before the rollout.
Send us the sample part and the applicable standard, and we will assess the test method and configuration. The existing series is oriented to insulated hand tools; for other products the electrode arrangement, test conditions and acceptance requirements need to be confirmed separately.
The international baseline for insulated hand tools is IEC 60900 (current edition 2018, with corrigenda issued in 2019 and 2020). Europe adopts it through CENELEC as an EN standard; Germany then publishes it as DIN EN IEC 60900, classified in the VDE body of standards as VDE 0682-201 (April 2019 edition, with a November 2020 corrigendum). German electrotechnical standards are produced by DKE, a joint organization of DIN and VDE that represents Germany in IEC and CENELEC — so German standards derive from IEC, not from US standards. The US counterpart product standard is ASTM F1505. When requesting a quote or placing an order, state the specified standard and edition, including year and corrigenda. Test conditions differ between editions, and the tester’s settings and delivery documents are confirmed against the edition you specify.
VDE certification of a hand tool assesses the tool itself and the manufacturer’s production control; it does not certify the test machine on the factory floor. The tester’s own electrical safety falls under a separate equipment standard (the IEC 61010 series) and is a different matter from whether the tool can be certified. When you prepare for a factory inspection, have three things ready for the test equipment: a calibration report within its validity whose range covers the test voltage and the pass/fail limits you actually use; a pre-use function check written into your quality procedures; and a traceable verification device for that check. Your certification body’s own requirements take precedence.
Under IEC 60900:2018 the two differ substantially. Type test (§5.5.3.1): the tool is first conditioned (§5.5.2), immersed in a water or steel-ball bath to 24 mm ± 2 mm from the nearest non-insulated part, and the voltage is raised at about 1,000 V/s (§5.5.1) to 10 kV rms at 50 or 60 Hz, held for 3 minutes, with leakage current measured. Alternative test after production (§5.5.3.2, for insulated hand tools): the tool manufacturer — that is, you — must show the same documented manufacturing procedure as the type-tested tool; no conditioning; 10 s from reaching the specified voltage; bath level 24 mm (+4/−2 mm); no leakage current measurement, so the verdict rests on whether puncture, sparkover or flashover occurs. In case of doubt, sampling under IEC 61318 using the type-test method applies. “10 seconds” therefore describes only the post-production alternative test, not the whole standard — and a 3-minute test cannot be costed on a production cycle time.
IEC 60900:2018 §5.5.3.1.1 requires the water bath to be replaced by a bath of 3 mm nickel stainless steel balls for tools capable of being assembled and for tools whose design does not allow testing in water. Tools assembled with square drives — sockets and extension bars, for example — may be tested as separate parts using dummies of the dimensions given in §5.5.3.1.2; parts tested this way do not need the complete assembly tested. That is where a steel-ball system earns its place, but the fixture, ball specification and immersion level still have to be checked clause by clause, which we do with you during selection — a tool fitting in the bath does not by itself make the method compliant.
In the type test, an insulated hand tool must draw less than 1 mA rms per 200 mm of insulation — IM = 5 L, with IM in mA and L the total insulation length in metres — so a tool with 200 mm of insulation is limited to 1 mA; hybrid tools must stay below 0.5 mA rms. Annex F of the standard gives worked examples. Pass/fail decisions therefore sit in the milliampere range. If you run type or sampling tests, the calibration report’s current points should cover that range rather than starting several milliamperes up, and the voltage points must cover 10 kV. The post-production alternative test does not measure leakage, so there the voltage calibration matters most. Unless otherwise stated, type-test values carry a ±5 % tolerance (§5.1). Put the intended test types, insulation length range and limits into the calibration requirement when you request a quote, and we will plan the calibration points accordingly.
Two approaches are common: a golden sample made from your own product with built-in known fault points, or a calibrated resistor box whose fixed high-precision resistors simulate pass and fail states. The resistor box is easier to send to an ISO/IEC 17025 accredited laboratory for annual calibration, gives a complete traceability chain and is more stable over time. Either way, the verification method belongs in your quality procedures and the verification device itself must be traceable; with a golden sample, auditors may ask for calibration certificates or a technical validation report for its internal components to confirm the fault states are consistent. How often to check is set by your own quality procedures.
Downloads and inquiry